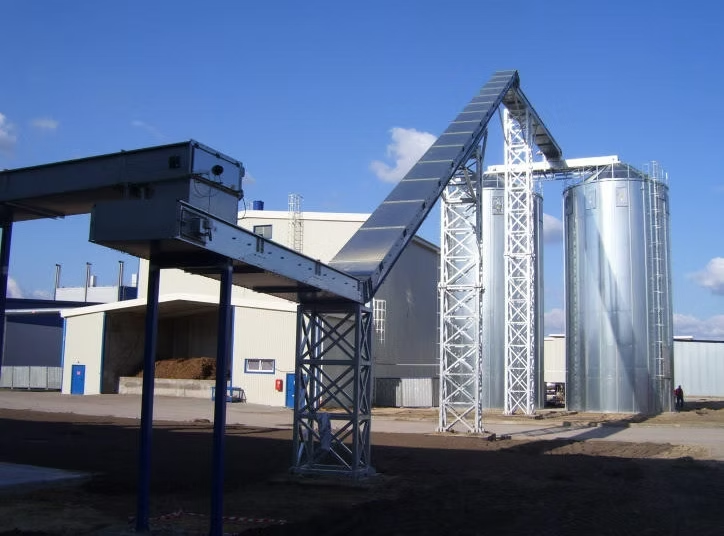
Project Overview
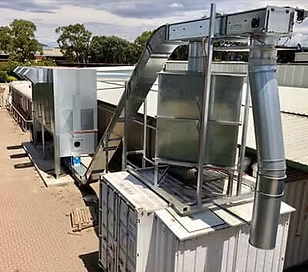
Australian Dust & Fume Control was engaged by a premier timber milling and timber processing facility in Mount Gambier to engineer, manufacture, and commission a high-capacity turnkey reverse-pulse dust extraction system. The facility operates multiple high-speed moulders, automated multi-rip saws, and continuous sanding lines, producing substantial volumes of fine combustible wood dust.
The Engineering Challenge
The previous legacy extraction setup suffered from severe static pressure drop across extended duct runs, resulting in dust settlement on elevated equipment surfaces and operator breathing zones. In addition, the system required full compliance with AS/NZS 4745:2012 (Code of practice for handling combustible dusts) with certified explosion-relief venting and spark detection isolation.
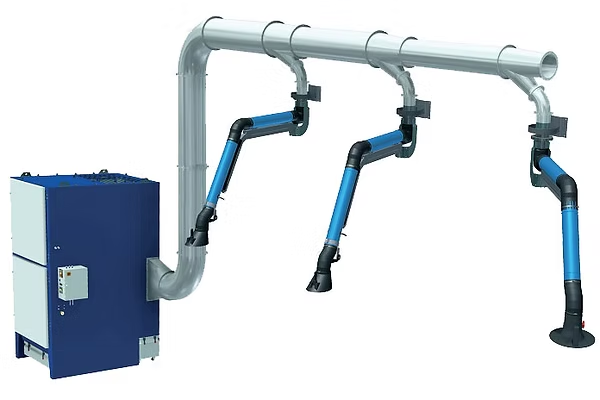
Our Engineered Solution
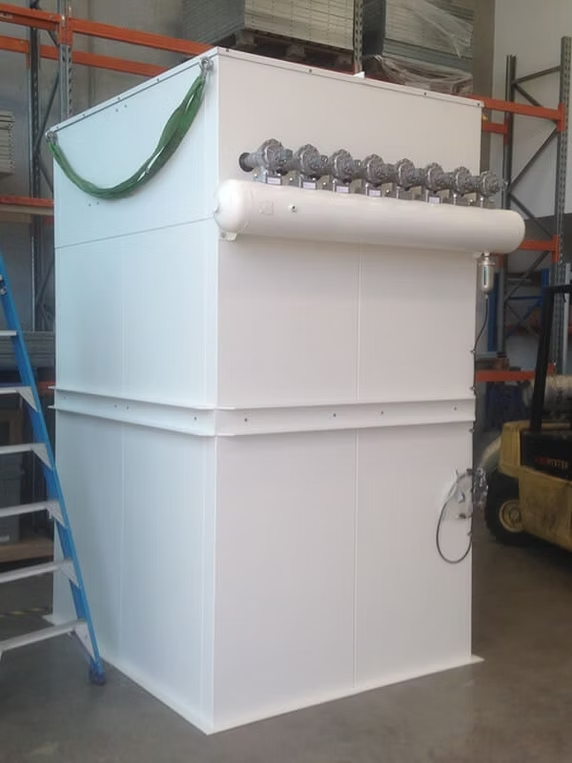
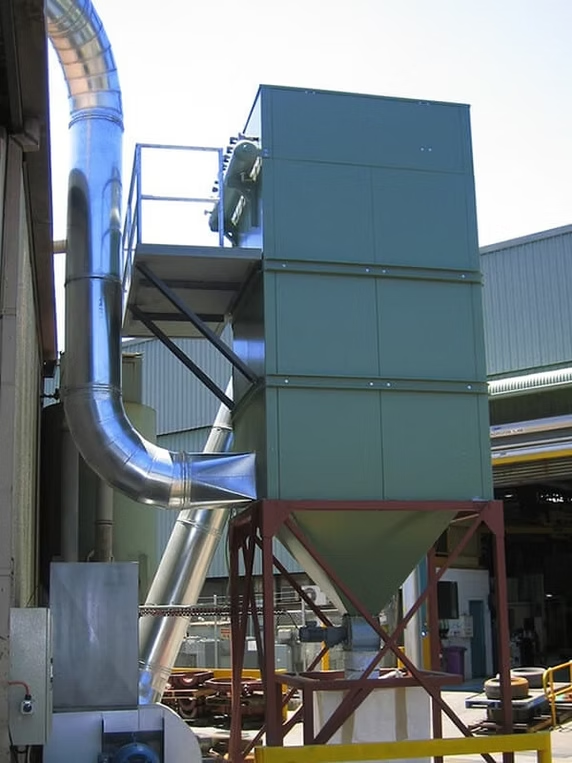
ADFC delivered a comprehensive industrial turnkey installation incorporating a heavy-duty modular Reverse Pulse Baghouse Collector rated for continuous 48,000 m³/hr airflow. Key engineering highlights include:
- Modular Pulse-Jet Baghouse: Premium anti-static polyester needle felt filter bags with integrated Venturi nozzles for online automatic pulse cleaning.
- High-Efficiency Backward-Inclined Fan: Heavy-duty dynamically balanced impeller driven by an energy-efficient 55kW TEFC motor with VFD smart speed control.
- ATEX/AS Compliant Explosion Mitigation: Flameless explosion vents, fast-acting mechanical abort gates, and high-sensitivity optical infrared spark detection and water quench system.
- Rotary Airlock & Waste Transfer: Continuous automated discharge into an enclosed pneumatic waste conveyor leading to the facility biomass storage silo.
Commissioning & Outcome
Comprehensive baseline air quality monitoring conducted post-commissioning recorded fugitive airborne particulate concentrations below 0.5 mg/m³—well within Safe Work Australia workplace exposure thresholds. The client reported a 32% reduction in facility maintenance downtime and significantly improved visual air clarity across all processing bays.