High-Efficiency Automated Filtration
Reverse Pulse
Baghouses
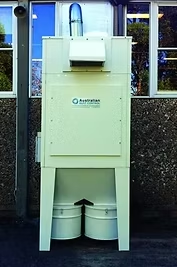
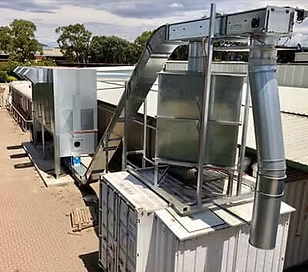
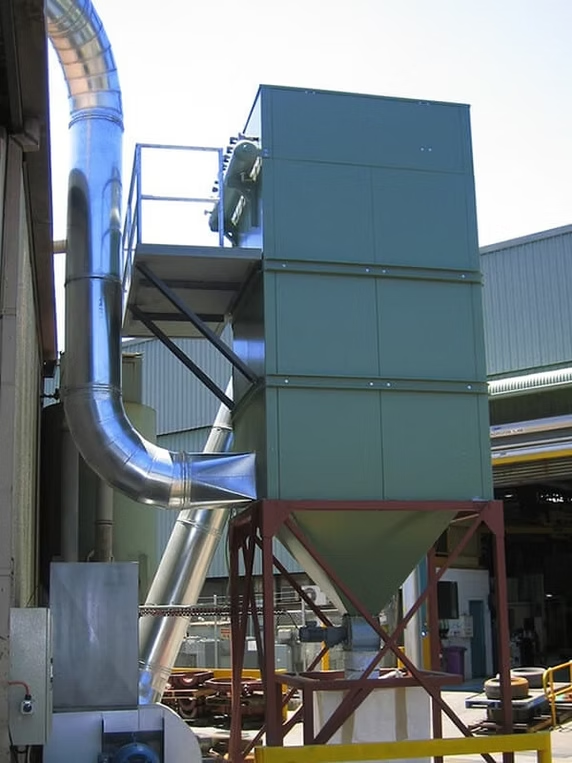
ADFC Reverse Pulse Baghouses (Pulse Jet Collectors) represent the industry standard in high-efficiency industrial air filtration, delivering continuous sub-micron particulate capture for heavy-duty facilities.
Australian Dust & Fume Control custom-engineers quality reverse pulse dust collectors tailored specifically to your facility. By engineering a solution matched precisely to your particulate characteristics, airflow volume, and floor plan, your workforce will enjoy a clean, hygienic workplace compliant with Safe Work Australia and EPA clean air standards.
Utilizing microprocessor-controlled solenoid pilot valves, high-pressure compressed air pulses (5 to 6.5 bar) are injected through precision venturi nozzles directly down each tubular filter bag. This supersonic pulse expands the fabric instantly, dislodging accumulated dust cakes into the hopper while the collector remains 100% online.
- 100% continuous online filtration with zero interruption to factory production
- Intelligent differential pressure pulse sequencer cleaning strictly on demand
- Walk-in clean air plenum allowing rapid, tool-less top-removal filter bag changes
- Full AS/NZS 4745 explosion relief venting with certified flameless indoor vents
< 2 mg/m³ Guarantee
Safe Work Australia Compliant
Equipment Parameters
Technical
Specifications
Standard parameters and engineered options available across our Australian-made equipment range.
| Parameter | Engineering Specification & Standard |
|---|---|
| Airflow Capacity | 2,000 to 200,000+ m³/h (Modular expandable cells) |
| Filtration Media | Needle felt polyester, anti-static stainless scrim, PTFE membrane |
| Compressed Air Supply | 5.0 – 6.5 bar clean, dry, oil-free compressed air |
| Emission Guarantee | < 2 mg/m³ compliant with EPA and Safe Work Australia standards |
| Structure Rating | Engineered for ±5,000 Pa to ±10,000 Pa static pressure |
| Controls | PLC touch screen or solid-state pulse sequencer with DP transducer |
Industry Sectors
Relevant Industries
& Applications
Delivering field-proven particulate collection solutions across Australia's primary industrial manufacturing sectors.
CNC Woodworking & Joinery
Chemical & Pharmaceutical
Metal Grinding & Blasting
Food & Dairy Powders
Plastics & Composites
Recycling & Waste Sorting
Require a Custom Reverse Pulse Baghouses Proposal?
Speak directly with our senior application engineers in Wetherill Park, NSW. We provide obligation-free site assessments, airflow sizing calculations, and formal turnkey proposals.