Continuous Heavy-Duty Filtration
Reverse Air
Baghouses
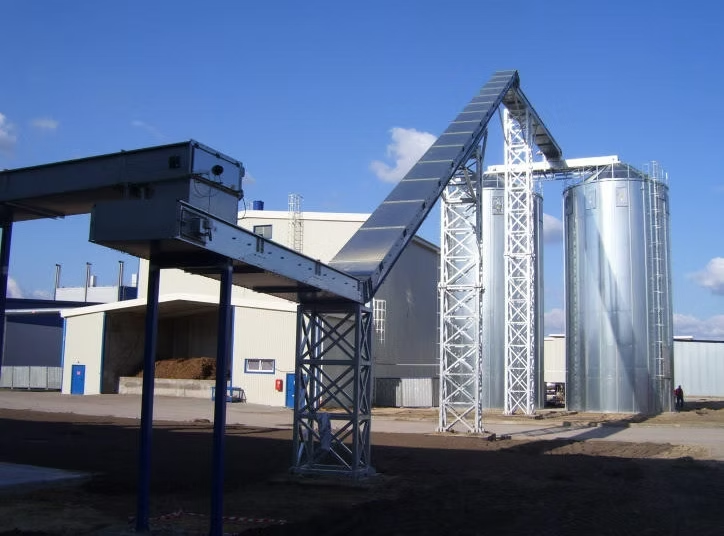
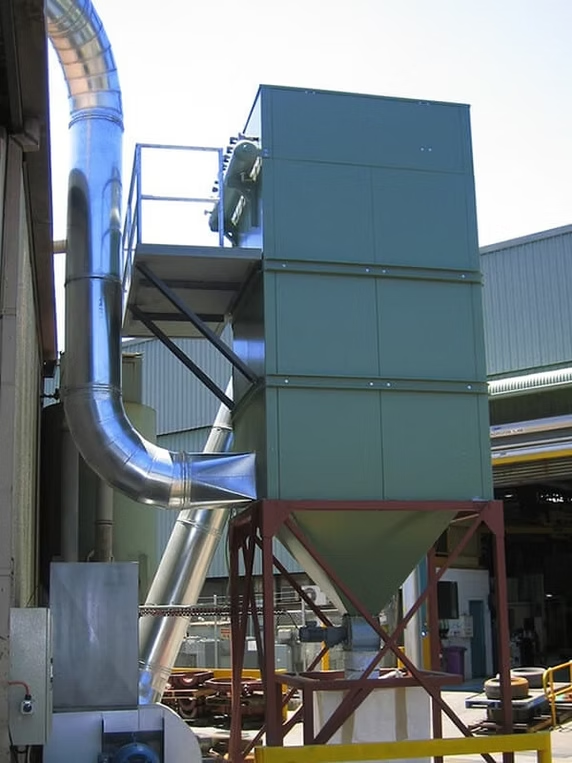
ADFC Reverse Air Baghouses are engineered for continuous, high-volume industrial operations where heavy dust loadings and high temperatures preclude compressed air pulsing.
Australian Dust & Fume Control is the Australian agent for Danish-designed Aagaard A/S Filter Units. The Reverse Air Baghouse dust collector is completely modular, providing industrial plants the flexibility to expand filtration capacity as production demands increase.
Operating under positive or negative pressure, cleaning is executed by a dedicated reverse air fan that gently deflects filter bags without mechanical shock. Because cleaning forces are evenly distributed along the entire bag length, fabric fatigue is virtually eliminated—substantially extending filter media lifespan up to 3–5 years even under abrasive silica, grain, and timber offcut duty cycles.
- Continuous multi-compartment offline cleaning without production downtime
- Gentle reverse airflow prevents mechanical fabric shock and premature bag tears
- High-temperature capability up to 260°C with Nomex, PPS, and PTFE filter media
- Zero compressed air required, cutting plant energy consumption and piping costs
99.9% Efficiency
AS/NZS 4745 Compliant
Equipment Parameters
Technical
Specifications
Standard parameters and engineered options available across our Australian-made equipment range.
| Parameter | Engineering Specification & Standard |
|---|---|
| Airflow Capacity | 5,000 to 150,000 m³/h (Modular expandable cells) |
| Filtration Efficiency | 99.9% particulate capture down to 1 micron (< 5 mg/m³) |
| Operating Temperature | Ambient up to 260°C (Nomex/PTFE Media) |
| Differential Pressure | 750 – 1,250 Pa normal operational range |
| Housing Construction | 3mm to 6mm laser-cut Mild Steel or 304/316 Stainless Steel |
| Explosion Protection | Certified AS/NZS 4745 burst panels or flameless indoor vents |
| Hopper Discharge | Motorized rotary airlock, screw conveyor, or manual slide gate |
Industry Sectors
Relevant Industries
& Applications
Delivering field-proven particulate collection solutions across Australia's primary industrial manufacturing sectors.
Timber & Sawmills
Grain & Bulk Agriculture
Asphalt & Kiln Dryers
Foundry & Smelting
Mining & Minerals
Cement & Lime Plants
Require a Custom Reverse Air Baghouses Proposal?
Speak directly with our senior application engineers in Wetherill Park, NSW. We provide obligation-free site assessments, airflow sizing calculations, and formal turnkey proposals.